Low-Volume Manufacturing: Best Options for 10–1,000 Parts
The 10-to-1,000-part range is an awkward middle ground. It's too many parts to comfortably print or machine one at a time, but rarely enough to justify a hardened production injection mold. This is exactly where the right process choice saves serious money — and it happens to be Flatout's sweet spot. Here are your best options and where each one makes sense.
CNC Machining
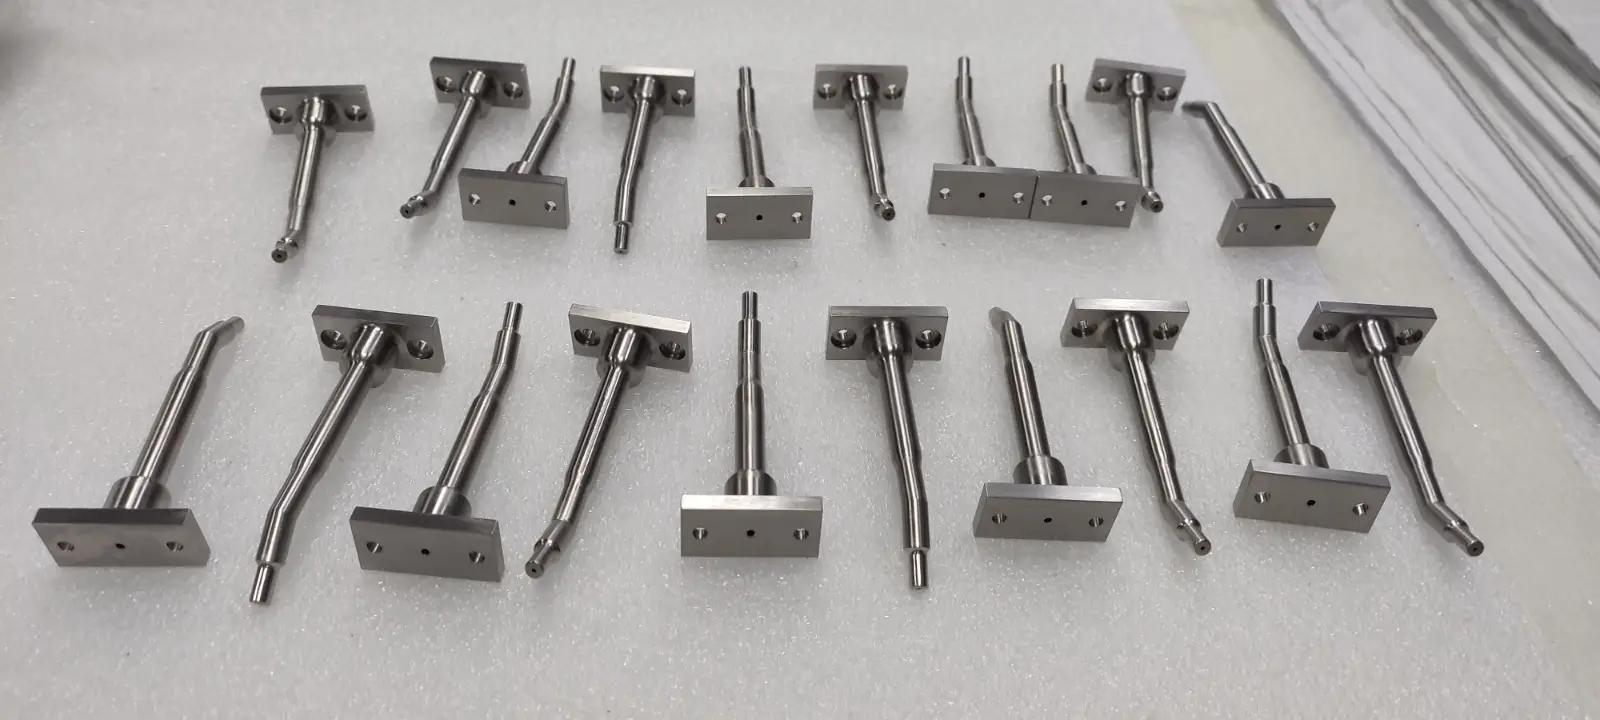
For low-volume metal or high-performance plastic parts, CNC is often the most direct path. Once a program is written and the part is fixtured, additional units come off relatively quickly, so per-part cost drops as quantity climbs. Strong from a handful up to a few hundred parts, especially when tolerances or material properties rule out printing.
MJF / SLS
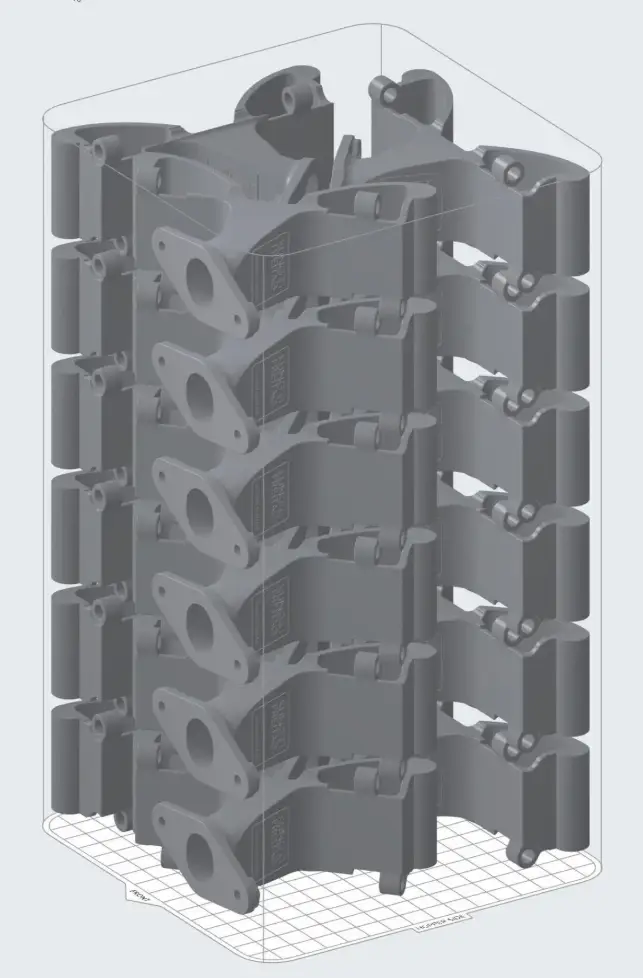
Powder-bed printing shines for low-volume plastic parts because you can nest dozens or hundreds of parts in a single build with no tooling cost. For complex geometries in the tens-to-low-hundreds range, MJF and SLS are frequently the cheapest and fastest option — and there's no break-even tooling investment to recover.
Urethane (Vacuum) Casting
Need 25–100 parts that look and feel like molded plastic without molding tooling cost? Urethane casting is the answer. You create a master pattern (usually SLA-printed), build a silicone mold around it, and cast production-like polyurethane parts. Materials can mimic everything from rigid ABS to soft rubber. The silicone mold wears out after a few dozen to ~100 pulls, which sets the upper limit.
Soft Tooling (Aluminum / Low-Cavity Molds)
When you're heading toward real injection-molded parts but don't want the cost of a hardened production tool, soft tooling bridges the gap. Aluminum molds are faster and cheaper to cut than hardened steel and are good for thousands of parts — ideal for bridge production while a production tool is built, or for a product whose lifetime volume never justifies hard tooling.
Where the Break-Even Quantities Fall
Roughly speaking: under ~25 parts, print or machine directly. From ~25–100 cosmetic or production-feel parts, urethane casting is often cheapest. From ~100–1,000+ identical plastic parts, soft/aluminum tooling starts to win as the tooling cost spreads across the run. For metal parts at any of these volumes, CNC usually leads unless the geometry forces metal 3D printing.
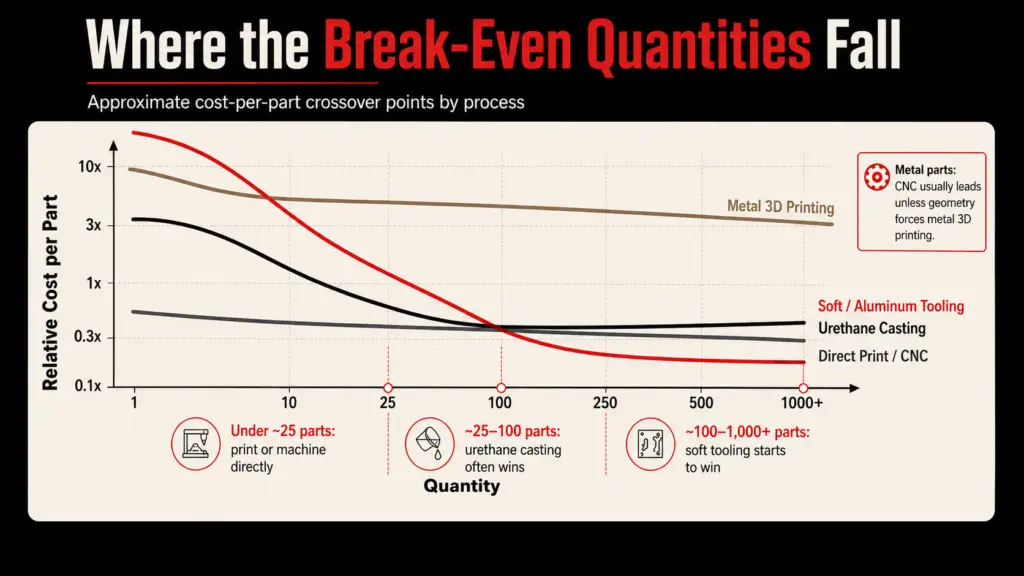
These crossover points shift with part size, complexity, and material — which is why the real answer comes from running your specific part through the numbers.
Find Your Sweet Spot
Low-volume is what we do. Tell us your part and your quantity and we'll model the options — direct machining, powder-bed printing, urethane casting, or soft tooling — and show you the most cost-effective route for your run size.